A steel member reaching the jobsite with the wrong hole pattern, an incorrect connection plate, a dimensional problem, or a weld issue creates more than a fabrication problem. The issue now sits in the middle of an active construction site, where correction becomes more complicated and expensive because erection crews, cranes, inspectors, engineers, and other trades might already be depending on the steel.
An erection crew might need to stop work while the condition receives review. A crane might remain idle or move to another area. Engineers might need to evaluate a proposed repair, while field crews bring welding equipment, lifts, tools, or replacement material into an area never intended for fabrication work. Coatings might require repair after cutting or welding, and surrounding work might also lose valuable schedule time while the steel issue gets resolved.
Strong steel fabrication quality control helps reduce those risks by identifying problems while the work remains in the shop, where trained personnel, fabrication equipment, inspection tools, documentation, and controlled processes are readily available. Effective quality control includes much more than a final inspection before steel leaves the facility. The process starts with project requirements and material identification, then continues through cutting, fitting, welding, dimensional verification, coatings, documentation, staging, and shipment.
At Mid-City Steel, quality is part of the fabrication process from the beginning. The objective is straightforward. Find issues where investigation and correction are easier, before they become field modifications affecting labor, equipment, safety, cost, and schedule.
Why Field Modifications Become Expensive So Quickly
Steel fabrication takes place in an environment designed for steel work. Fabricators have shop cranes, welding stations, fixtures, automated equipment, inspection tools, current drawings, quality personnel, and direct access to the teams responsible for production. When an issue appears during fabrication, those resources help the team evaluate the problem and determine the appropriate next step without disrupting an active erection site.
The jobsite presents a different environment. An erector dealing with a fabrication issue might be working several stories above grade, with access requiring a manlift or specialized rigging. A member might already support surrounding framing, while other components block the area needing correction. Temporary support might be necessary before work proceeds, and weather, congestion, limited power, restricted hot work, or nearby trades might add complexity.
Even a relatively small discrepancy often starts a chain of activity. The erector identifies the issue and stops the affected work, the contractor documents the condition, the fabricator reviews drawings and production information, and the engineer determines whether a proposed repair meets design requirements. Replacement material might require fabrication and delivery, while field welding or drilling might require additional inspection and coating repair. The physical repair might take only a few hours, yet the surrounding disruption might affect several crews and several days of work.
Quality control focuses on preventing avoidable versions of those situations before fabricated steel leaves the shop.
Quality Starts Before Fabrication Begins
Some quality problems begin long before steel reaches a saw, drill line, robotic processing system, fitting station, or welding area. An outdated drawing revision, misunderstood specification, incorrect material grade, missed finish requirement, or unresolved connection detail creates risk before production begins. Once fabrication moves forward using incorrect information, each additional operation increases the amount of work affected.
A strong quality process therefore begins with project information. Approved drawings need clear revision control, while project specifications need review for special inspection requirements, welding procedures, material grades, coating systems, dimensional tolerances, testing requirements, and documentation expectations. Those requirements need to reach the people responsible for purchasing, detailing, production, inspection, coatings, and shipping.
Current information becomes especially important in a digitally connected fabrication operation. Detail models, shop drawings, machine data, work orders, inspection records, and production systems all need to remain aligned. Automation improves speed and repeatability, yet fast equipment also processes incorrect information efficiently when controls break down. A wrong hole location or outdated connection detail repeated across multiple pieces quickly turns one information problem into a much larger production problem.
Controlled project information provides the first line of defense because quality starts with building the correct piece from the correct requirements.
Material Traceability Protects the Starting Point
A finished beam often looks like any other beam of the same size, but its material documentation tells a more complete story. Structural steel projects specify material grades based on design requirements, while certain projects add toughness, testing, domestic sourcing, fracture-control, or other material requirements. Plate thickness, heat number, grade, and supporting mill documentation also become important depending on the application.
Material traceability connects the steel entering the fabrication facility with the requirements of the project. The process starts when material arrives, when receiving personnel verify shipments against purchase information and supporting documentation. Required identification then needs to remain connected to the material as stock moves through storage and fabrication.
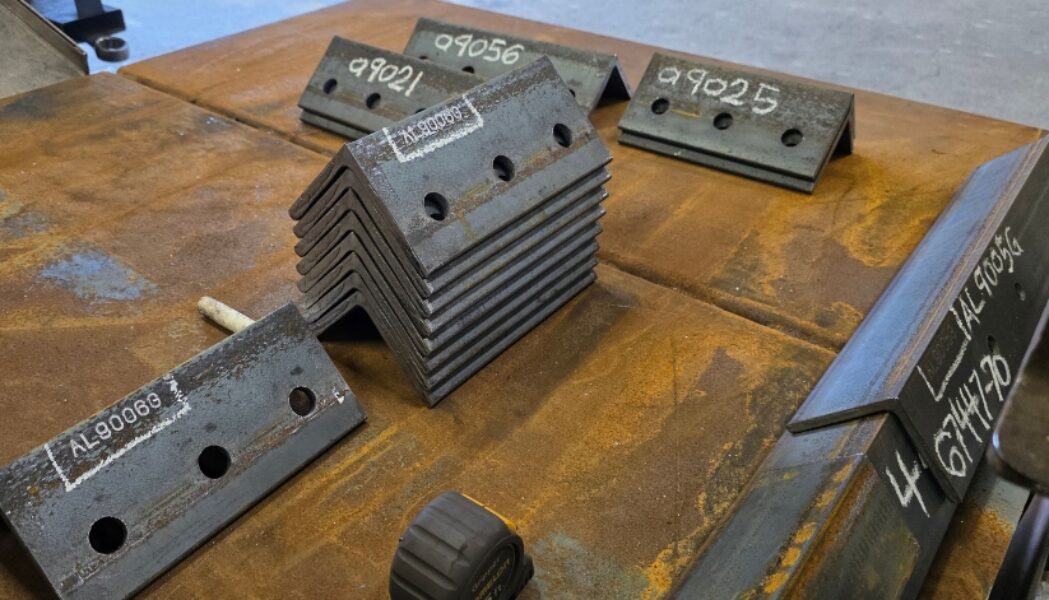
Traceability becomes more involved when one piece of stock turns into several fabricated parts. A plate might produce connection plates, stiffeners, gussets, base plates, and other components, so procedures need to preserve required identification as material gets cut and distributed through production.
This control becomes especially valuable if a question develops later about material grade, heat information, or project compliance. Reliable records help the team establish which material went into a fabricated component and support the documentation associated with the work. Without strong traceability, answering the same question might require additional investigation, testing, replacement, or delay.
Dimensional Checks Protect Fit-Up
A fabricated steel member rarely works alone. Beams connect to columns, braces connect to gusset plates, base plates align with anchor rods, stairs meet landings, platforms connect to framing, and equipment supports line up with machinery. Small dimensional differences therefore influence far more than one individual piece.
An incorrect member length affects alignment, while a misplaced hole affects bolted fit-up. An incorrectly located connection plate shifts the next member, and a base plate pattern failing to match anchor rods creates an immediate erection problem. A stair landing at the wrong elevation affects surrounding finishes, access, and adjacent construction.
Dimensional quality control verifies critical measurements throughout production rather than waiting until every operation is complete. Depending on the component and project requirements, inspectors and production personnel might verify overall length, hole locations, plate dimensions, connection locations, assembly geometry, squareness, camber, sweep, bolt patterns, elevations, or other important dimensions.
Timing matters as much as the measurement itself. Checking a connection location before extensive welding gives the team more options than finding the same issue after welding, blasting, coating, and loading. First-piece checks also help identify setup concerns before the same operation repeats across a larger production run.
Mid-City Steel uses advanced fabrication equipment to support consistent cutting, drilling, marking, and processing, while quality personnel verify finished work against project requirements. Precision equipment supports accurate production, and inspection confirms whether the fabricated result matches the approved information.
Fit-Up Checks Catch Problems Before Welding
Fit-up represents another important quality checkpoint because welding permanently joins components and makes later correction more involved. Before welding begins, fabricators need to confirm pieces are assembled in the intended position, with plate location, joint geometry, gaps, alignment, orientation, and connection dimensions matching project requirements.
A plate installed on the wrong side of a member might seem like an obvious error after completion, yet the best time to identify the problem is before welding starts. The same principle applies to reversed pieces, incorrect stiffener locations, connection offsets, joint preparation concerns, and dimensional inconsistencies between parts.
Fit-up inspection gives the team an opportunity to correct an assembly while rework remains limited. Once welding begins, weld removal requires additional labor and care, while affected material might need evaluation and further inspection. Rework also introduces added heat and potential distortion, which increases the amount of attention required before the assembly returns to normal production.
Finding the same issue after shipment raises the cost and complexity again. In-process fit-up checks keep corrections at the earliest practical stage.
Welding Procedures Create Consistency
Structural welding does not depend on individual preference. Welding procedures establish approved variables for producing specified joints, including process, joint design, filler material, position, preheat, electrical variables, and other requirements connected to the work. Qualified welders and welding operators perform work within those established procedures.
This structure creates repeatability because welding personnel work from documented requirements tied to applicable codes, project specifications, and approved procedures. Quality control supports welding before, during, and after the weld itself.
Before welding, the team reviews fit-up, joint preparation, material condition, procedure requirements, and access. During production, welding personnel follow established procedures and monitor the work. After welding, inspection verifies the completed joint according to applicable requirements. Some projects also require nondestructive testing beyond visual inspection, depending on the design, specification, connection type, code requirements, and project quality plan.
The objective remains consistent throughout the process. Identify unacceptable conditions before the steel reaches the field, where access, schedule pressure, and surrounding construction make repair more difficult.
Weld Inspection Is More Than Looking for Obvious Defects
Visual weld inspection requires trained personnel who understand the requirements being evaluated. Inspectors review factors such as weld size, length, profile, location, continuity, and visible discontinuities, while also verifying whether the completed weld matches approved fabrication information.
Appearance alone does not determine compliance. A smooth-looking weld still needs the correct size, length, location, process, and supporting documentation. At the same time, a structural weld does not need ornamental appearance unless the project includes specific visual requirements.
Inspection keeps those expectations tied to project documents and applicable standards. Finding a weld concern in the fabrication facility gives the team controlled access for evaluation and repair, with tools, personnel, drawings, and inspection resources nearby. Finding the same concern after erection might require lifts, scaffolding, field welding equipment, fire protection, weather planning, and another inspection visit.
The fabrication shop remains the better environment for resolving the issue.
Why In-Process Inspection Matters More Than One Final Check
Final inspection remains an important step before finished steel receives approval for shipment, but final inspection should confirm the work rather than serve as the first serious quality review.
Consider a complex welded assembly moving through several operations. Material gets cut, holes receive processing, plates get fit, components are welded, the assembly receives dimensional verification, surface preparation follows, a coating system gets applied, and the finished piece then moves into staging and shipping.
Waiting until the end creates unnecessary risk because some features become harder to access after assembly, while welded components might hide surfaces visible earlier. Coatings cover fabrication surfaces, large assemblies become harder to reposition, and any rework risks damaging completed finishes after significant labor has already gone into the piece.
In-process inspection places quality checks where they provide the greatest value. Material receives verification before fabrication, processed pieces receive dimensional checks, fit-up gets reviewed before welding, welds receive inspection before later operations cover or restrict access, completed assemblies receive dimensional verification before finishing, and coatings receive their own preparation and inspection controls.
Each checkpoint helps prevent an issue from traveling farther downstream, where correction becomes more difficult and expensive.
Documentation Creates an Audit Trail
Quality work also needs organized records connecting physical fabrication with the procedures, materials, inspections, and requirements behind the finished component. Depending on project requirements, documentation might include material certifications, receiving information, welding procedure documentation, welder qualifications, inspection reports, nondestructive testing results, dimensional checks, coating records, calibration records, nonconformance reports, and corrective actions.
Good documentation serves several practical purposes. Records confirm required steps took place, give project teams reliable information when questions arise, and establish accountability for inspections, approvals, material identification, and corrective action. Instead of relying on memory, teams review documented production history and current project information.
Documentation also supports continuous improvement. When similar issues appear more than once, records help quality and production teams identify patterns and investigate where additional training, equipment attention, process changes, or clearer information might improve future work.
The value extends far beyond paperwork. Records help turn quality control from a collection of individual habits into a repeatable system.
Nonconforming Work Needs a Defined Process
Quality control does not mean every fabricated piece moves through production without an issue. Steel fabrication involves complex information, material, equipment, welding, handling, and human decisions, so unexpected conditions sometimes appear.
A strong quality system defines what happens when work fails to meet a requirement. The condition receives identification and control, the team evaluates the issue, the appropriate disposition gets determined, required engineering or customer approval gets obtained, and repair or rework receives verification before the piece proceeds.
This process prevents informal fixes from bypassing project requirements. Some changes affect structural design intent, so a fabricator should not alter a structural detail independently when engineering review is required. A controlled nonconformance process routes the issue to the appropriate authority and creates a record of the decision.
Early detection gives the project team more options. When an issue appears during fabrication, the team often has immediate access to drawings, engineers, material, equipment, inspectors, and production personnel. Once the same issue reaches the jobsite, every decision takes place under greater schedule pressure and with fewer convenient resources.
Coating Inspection Protects Completed Fabrication
Quality control continues after dimensional work and welding are complete because coating systems introduce another group of requirements involving surface preparation, cleanliness, environmental conditions, film thickness, cure, and final appearance.
A correctly fabricated member still creates problems when a coating prevents proper connection, receives damage before delivery, or fails to meet project requirements. Surface preparation therefore needs verification before coating application, while environmental conditions might require monitoring during application and dry film thickness might need measurement after each specified stage.
Finished steel also needs handling methods suited to the coating system during staging and shipment. Chains, dunnage, lifting methods, stacking arrangements, and repeated movement all influence the condition of the finished surface.
When coating problems receive attention in the shop, repairs occur in a more controlled environment. Field coating repairs usually involve more difficult access and greater environmental variability, which gives another reason to treat coating inspection as part of the overall fabrication quality process.
Quality Continues Through Staging and Delivery
A fabricated member has not successfully completed the quality process simply because production has ended. Steel still needs identification, staging, loading, securement, transportation, and unloading before installation begins.
Piece marks need to remain clear, loose connection material needs organization, loads need proper support, and coated surfaces need protection from avoidable handling damage. Shipping documents also need to match the material on the trailer so field crews know what arrived and where each piece belongs.
Delivery sequence affects quality in a practical sense as well. Steel arriving in the wrong order might require extra unloading, movement, and restaging, and every additional handling step increases the opportunity for coating damage, misplaced loose parts, or piece-mark confusion.
Quality therefore extends into logistics because the objective involves more than producing compliant steel. The steel also needs to reach the jobsite in a condition and sequence supporting efficient field installation.
The Cost of Prevention Is Lower Than the Cost of Field Rework
Inspections, documentation, dimensional checks, material traceability, and controlled procedures all require time, but those activities provide value when they prevent a field problem involving multiple crews and expensive equipment.
Correcting a connection plate during shop fit-up might involve a controlled adjustment with fabrication equipment nearby. Correcting the same plate after erection might involve a crane, manlift, engineering review, field welding, additional inspection, coating repair, and disruption to the erection sequence.
The same principle applies to incorrect hole patterns, material questions, welding issues, missing attachments, coating deficiencies, and dimensional problems. Finding an issue before shipment keeps the correction inside the fabrication workflow. Finding the same problem while ironworkers and a crane wait on the jobsite changes the cost quickly.
The value of quality control therefore reaches beyond reducing scrap or rework inside the shop. Strong systems help protect crane time, erection productivity, delivery schedules, inspection schedules, project coordination, and work by other trades.
Quality Control Supports Predictable Field Performance
Contractors and erectors need steel ready for installation because the jobsite already contains enough variables. Weather changes, site access shifts, concrete tolerances affect fit, other trades compete for space, crane schedules move, and delivery windows change. Fabrication errors add another variable, one project teams work hard to reduce.
Steel fabrication quality control provides a structured approach. Material traceability verifies the correct steel enters the process, dimensional checks protect geometry and fit-up, welding procedures establish repeatable requirements, inspection verifies completed work, and documentation provides accountability. In-process checkpoints identify problems before additional work makes correction harder.
No quality system eliminates every challenge from a complex steel project, but a disciplined process reduces the number of preventable problems traveling from the fabrication shop to the erection site.
For Mid-City Steel, quality is not a final step added before shipment. Quality runs through the entire fabrication process, from project information and material control through cutting, fitting, welding, dimensional inspection, coatings, staging, and delivery. This approach supports the outcome customers care about most, steel arriving ready for the next phase of the project.
Planning a structural, miscellaneous, industrial, bridge, or complex steel fabrication project? Talk with Mid-City Steel about your project requirements, quality-control needs, fabrication scope, and delivery schedule.